Sourcing an EVA case goes wrong in two directions: procurement teams either settle for generic stock cases that let high-value equipment shift in transit, or they specify foam density and shell hardness they cannot verify, and warranty claims follow.
This guide covers what an EVA case is, how it is molded and stitched, the main types, realistic protection levels, the custom versus standard cost split, and a factory audit sequence you can run before releasing bulk funds.
EVA 케이스는 무엇입니까?
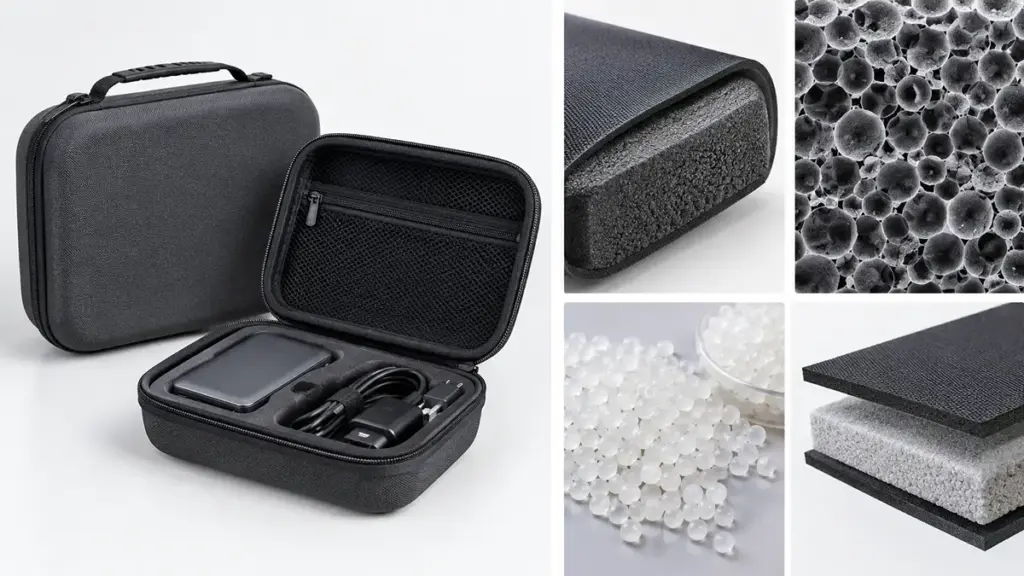
An EVA case is a semi-rigid, lightweight protective enclosure that bridges the gap between soft fabric bags and heavy hard-shell plastic cases.
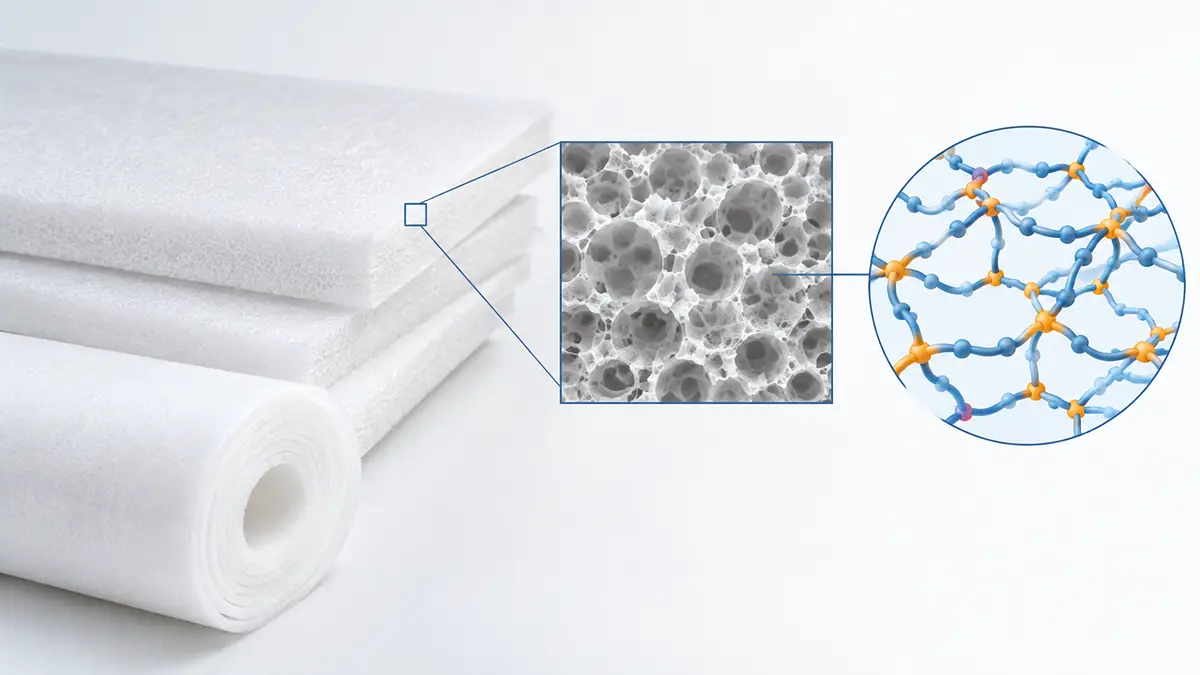
에틸렌-비닐 아세테이트 (에바) is a thermoplastic copolymer produced by blending ethylene and vinyl acetate to achieve customizable levels of flexibility and resilience. Unlike open-cell foams that act like sponges, the closed-cell structure of EVA contains sealed air pockets that absorb physical shocks and resist moisture penetration, keeping contents isolated from external hazards.
Key Material Characteristics
EVA combines the impact protection of rigid hard-shell plastics with the lightweight flexibility of soft fabric bags: the shell bends under pressure rather than cracking. It stays flexible in cold environments and recovers its shape after moderate compression, which prevents permanent deformation under typical transport conditions.
Primary Structural Designs
Manufacturers shape these enclosures into two functional families:
- Molded hard-shell configurations: thermoformed custom upper and lower shells joined by a high-durability zipper.
- Organizer and custom-insert designs: precision die-cut foam, 메쉬 포켓, and elastic straps that secure specific equipment parts and prevent internal shifting.
Protective Capabilities and Limits
For everyday handling, EVA provides reliable protection against routine drops, 진동, surface abrasion, and dust. But know the limits: standard configurations are not natively waterproof or crushproof. Equipment operating in extreme environments requires additional polyurethane coatings, waterproof zippers, gasketed seals, or rigid internal reinforcements.
How EVA Cases Are Manufactured
Manufacturing custom EVA cases follows a controlled sequence: CAD design, material lamination, 절단, pre-heating, 압축 성형, 트리밍, 스티칭, 점검, 그리고 포장.
Every molded EVA case is a three-layer composite. A sandwich lamination bonds an exterior protective textile (oxford nylon such as 600D/1680D, ballistic nylon, 또는 PU 가죽), a central semi-rigid EVA core, and a soft interior lining (velvet, microfiber, or brushed tricot). Strict control over adhesive coating weight, heat activation temperature, and cooling time prevents air pockets and surface bubbling in later molding phases.
From Flat Sheet to Formed Shell
- Design and material selection: engineers translate physical product dimensions into 3D CAD models that factor in cooling shrinkage, mold draft angles, and lining thickness, then specify the EVA sheet grade for density, Shore hardness, and shock-absorption limits.
- Lamination: factories bond exterior textiles and soft interior linings to the raw EVA core using heat-activated adhesives.
- 절단: hydraulic or steel-rule die presses punch flat laminated blanks slightly larger than the final part footprint.
- 예열: blanks pass through ovens or infrared tunnels until the copolymer softens; underheating prevents full mold conformation and overheating damages the adhesive bond, so technicians monitor the curve closely.
- Molding: operators place the hot blank into matched, CNC-machined aluminum molds, and hydraulic presses (typically in the range of several tons to tens of tons) force the material into every rib and recess, followed by in-mold cooling to lock in geometry and prevent warping.
하드웨어, 스티칭, and Finishing
Trimming presses or CNC tools shear off excess perimeter material to create a clean sewing edge. Industrial sewing machines then attach coil, reverse-coil, or polyurethane-coated water-resistant zippers, perimeter binding tape, and handles directly to the molded flanges. High-stress zones such as D-rings, strap anchors, and corners take dual sewing lines or reinforced stitch patterns, and load anchors spread handle and strap forces across a broad area of the shell with internal backing plates or reinforced textile patches. One visible quality line is finishing: factories that treat an EVA shell like luggage, with leather-goods stitching, tend to outlast press-and-zip shops in the field.
In-Line Quality Checks
Before bulk packing, quality teams check the run for surface wrinkles, fabric delamination, and misaligned seams, and sample units undergo drop tests, zipper cycle trials, and handle pull tests. 브랜딩 (thermal debossing, silk-screen printing, or stitched rubber patches) is applied and verified against the buyer’s artwork as part of the same gate.
Types of EVA Cases and Uses
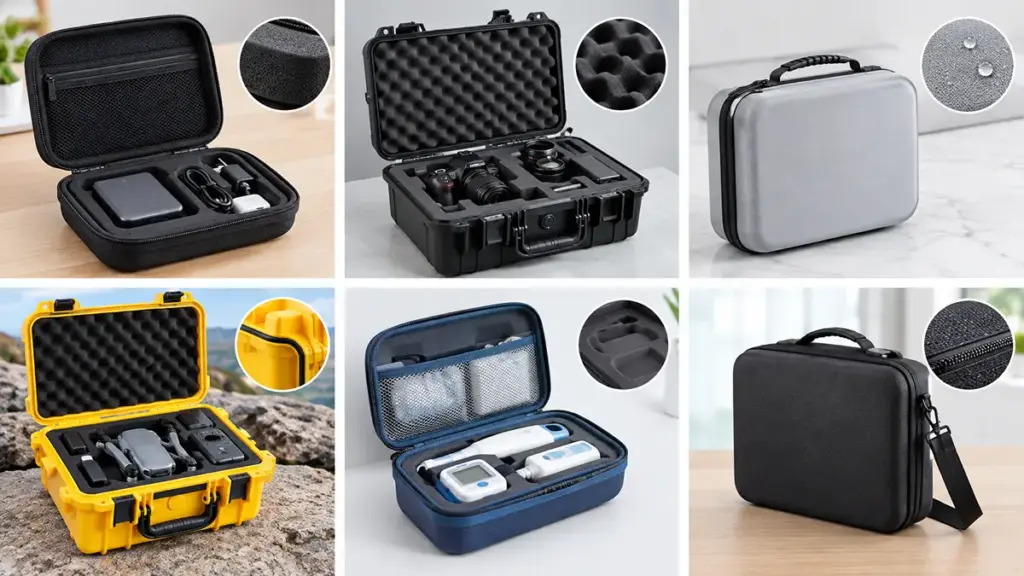
Selecting the right types of EVA cases means balancing shell rigidity, interior foam inserts, and cleanable exterior laminates against the equipment being protected.
Standard soft bags fail when drop protection is non-negotiable, while heavy hard cases add unnecessary shipping weight. Most buyers search for a “case for [device]” rather than by material name; translating device language into spec language before requesting quotes puts you in a different, faster conversation with factories.
Classification by Shell Construction
- Molded hard-shell and semi-rigid zipper cases: structural defense against high-impact forces, securing delicate electronics during rugged transit.
- Organizer and custom-molded options: dedicated interior compartments, 탄성 스트랩, and integrated mesh pockets that prevent accessories from shifting.
- Hybrid and display cases: EVA foam combined with rigid plastics, aluminum frames, or premium fabrics for retail presentation and industrial durability.
Target Industry Applications
- Consumer electronics and gaming: compact, zippered designs for travel accessories, premium headphones, VR headsets, and handheld consoles.
- Medical and healthcare: custom cases with cleanable exterior laminates protecting portable diagnostic sensors, surgical instruments, and field tools.
- 산업용, audio, and field operations: reinforced configurations isolating multimeters, microphones, and GPS units from harsh vibration.
Protection Levels and Materials
A high-performance EVA case matches foam density, shell hardness, and closure quality to the specific hazards of your transport environment.
Classification of Protection Levels
- Basic protective: shields accessories and cables from scratches and light drops with standard zipper closures.
- General-purpose: cushions cameras, hand tools, and medical devices through molded shells and medium-density interiors.
- Heavy-duty: resists severe industrial handling using reinforced corners and high-density foam inserts.
- 내후성: repels rain and splashes through coated textiles and water-resistant zippers.
- Immersion-rated: engineered toward ingress protection ratings such as IP67 using gasketed seals and airtight closures, verified by whole-unit testing.
Density and Hardness, Not Thickness
Product teams often assume thicker foam automatically means better protection. In reality, performance is a system: 밀도, durometer, wall geometry, and closure quality together decide how well a case survives. Case-grade EVA typically falls in the region of 30 에게 80 kg/m³ (the full commercial foam range runs far wider), with shell hardness expressed in Shore C and sitting in the firmer part of the scale. As one high-end benchmark, KinFish standardizes on 75 Shore C hardness over a 6 mm sheet, while a common regional trade norm is 65C over 5 mm.
Advanced designs rarely use a single uniform foam block: 부드러운, low-density contact layer against the product prevents surface abrasion, while a firmer, high-density support layer absorbs impact without bottoming out. Ask suppliers for compression set figures measured under recognized ASTM foam test methods rather than accepting hardness claims alone.
Shell, Closure, and Water Resistance
While raw closed-cell EVA naturally repels moisture, a bare shell never guarantees waterproof performance. Water penetrates standard zippers first, so true weatherproofing upgrades the entire closure system: reverse-coil water-resistant zippers, sealed seams, and compressed rubber gaskets. Do not rely on material certificates to claim certified ingress protection such as IP65 or IP67; that rating demands testing of the fully assembled case. For heavy industrial gear, rigid plates of ABS, 폴리카보네이트, or HDPE embedded in high-load panels distribute concentrated weight and prevent shell collapse when cases are stacked in transport.
Marketing claims like “shockproof” should be checked against standardized test frameworks, ~와 같은 ISTA transport simulation procedures or ASTM drop and environmental methods. For shell material choices in clinical settings, our comparison of hard plastic vs EVA medical cases covers the trade-offs in more detail.
Custom EVA vs Standard Cases
Choosing between custom EVA vs standard cases means balancing precision protection and branding against tooling budget and market speed.
Are you packaging high-value medical hardware, or simply shipping generic charging cables? That question should decide the path: custom tooling either pays back at volume, or it balloons your upfront engineering budget for nothing.
| Dimension | Custom-Molded EVA | Standard Stock Case |
|---|---|---|
| Fit and protection | Molded cavities immobilize the device; internal collision damage is engineered out | Generic pick-and-pluck foam degrades over time and allows internal shifting |
| 브랜딩 | Deep debossed logos, custom-dyed fabrics, molded zipper pulls | Surface screen printing, adhesive labels, stock colors only |
| Upfront cost | One-time tooling charge that amortizes per unit at volume; request a written, itemized mold cost | No tooling; a low-risk option for pilot runs or market tests |
| Timeline | Free design support with drawings in 2 날; samples in 10–15 days; bulk production in 30–35 days (KinFish figures) | Immediate dispatch for simple, in-stock geometries |
| Order volume | MOQ 1,000 units at KinFish; some market suppliers quote around 500 | Smaller lot purchases from catalog designs |
Low-volume runs favor stock options, but scaling up shifts the economics toward customized tooling, because the amortized mold cost per unit drops quickly at production quantities. Custom fabrication also lets technical designs specify heavy-duty walls, high-density shock-absorbing foam, and water-resistant closures tuned to your real transport hazards.
How to Vet an EVA Case Supplier
Evaluating a supplier on price alone exposes material density, 지퍼, and chemical compliance failure points. Audit manufacturing capacity and set measurable specifications in writing.
This section covers the audit itself. For a directory-level view of who operates in this space, see our roundup of top custom EVA case suppliers worldwide.
| Vetting Phase | Critical Metrics and Verification Methods |
|---|---|
| Legitimacy and capacity | On-site or third-party audits of thermoforming presses, sewing lines, and lamination machinery to filter out trading intermediaries. |
| Material quality | Verification of EVA foam density and Shore C hardness against your datasheet, plus compliance with REACH, 로스, and California Proposition 65. |
| Prototyping and testing | Staged progression from engineering prototype to first article; 낙하 테스트 (typically from around 1.2 m) and zipper cycle verification. |
| Commercial agreements | Defined Acceptable Quality Limits (AQL), mold ownership rights in writing, and staged payment schedules. |
Verifying Manufacturer Legitimacy and Production Capacity
How do you know if your prospective partner actually owns the machines, or operates from a shared desk? Request the business registration papers and compare the registered address with the actual production location; trading intermediaries typically obscure factory addresses or subcontract assembly without warning, causing lead-time delays in peak shipping seasons.
Conduct an on-site inspection or commission a third-party factory audit. On the shop floor, check lamination stations for uniform adhesive control, compression molding lines for temperature-controlled molds and adequately sized hydraulic presses, and sewing lines for consistent edge-trimming accuracy. How a plant stages raw materials matters too: sheets exposed to high humidity or unsystematic piles of finished parts predict dimensional warping and unpredictable quality.
Assessing Material Quality and Compliance
Many suppliers promise a “premium EVA case” without a single hard metric. Enforce exact specifications in your technical datasheet: foam density and Shore C range for your application, an agreed durometer tolerance band, and a compression set figure under a recognized test method. Chemical safety is another common failure point: ask for current, accredited third-party test reports (for example from SGS or TÜV) confirming REACH, 로스, and Proposition 65 규정 준수, matched to the exact material batch used for your run; a generic self-declared certificate proves little. Factories differ on how deep compliance goes — at KinFish, 도달하다- and RoHS-passing materials are the default specification, and the site holds an environmental impact assessment that is uncommon among regional peers.
Verify that the manufacturer runs batch traceability, tracking every lot of foam from compound formulation through completed assembly, so a field defect can be traced back to a production window.
Running a Strict Prototyping and Testing Sequence
Never transition directly from a 3D model to mass production. Follow a staged progression:
- Raw material samples: approve exterior fabric, 내벽, hardware, and foam sheets for texture and color consistency.
- Engineering prototypes: temporary tooling or CNC-cut foam verifies internal clearance, pocket fit, and ergonomics.
- First-article units: samples produced on the actual production-grade aluminum molds show final tolerances and structural integrity.
Subject prototypes to physical testing: drop tests from around 1.2 meters onto concrete across all faces, corners, and edges; high-temperature conditioning to confirm the lamination adhesive does not bubble; and repeated zipper and handle cycling to locate weak points early. Transport simulation protocols such as ISTA series or ASTM D4169 give you a repeatable framework for these checks.
Locking Quality Agreements and Commercial Terms
Draft quality agreements on the AQL framework with explicit defect classes: critical defects at AQL 0 (exposed sharp edges, loose handle stitching, misaligned closures), major defects at AQL 1.5–2.5 (severe wrinkles, visible glue marks, zipper binding, shell warping), and minor defects at AQL 4.0 (tiny cosmetic scratches, slight shade variation, loose threads).
Resolve tooling rights in writing: state that you own the aluminum molds and CNC files, define the supplier’s mold maintenance responsibility, and secure your right to transfer tooling to another factory if schedules slip. On payment, avoid full advance: 구조 30% upfront and 70% upon successful pre-shipment inspection, with late-delivery penalty clauses, so the factory stays accountable until the shipment clears your check.
From Approved Sample to Delivery
Once vetting passes, a disciplined purchase sequence protects the specification you just verified:
- RFQ and design review: share product dimensions or 3D files; expect the factory to flag mold feasibility and suggest fit optimizations.
- Sample approval: sign off on materials, 색상, 맞다, and stitching against a written spec sheet.
- Specification freeze: confirm configuration, 재료, hardware, logo artwork, 공차, and packaging in writing before bulk runs start.
- Production and pre-shipment inspection: check bulk output against the frozen spec and the approved golden sample, including AQL sampling.
- Delivery and after-sales: the balance releases after inspection passes; document defect handling terms before the first PO.
최종 생각
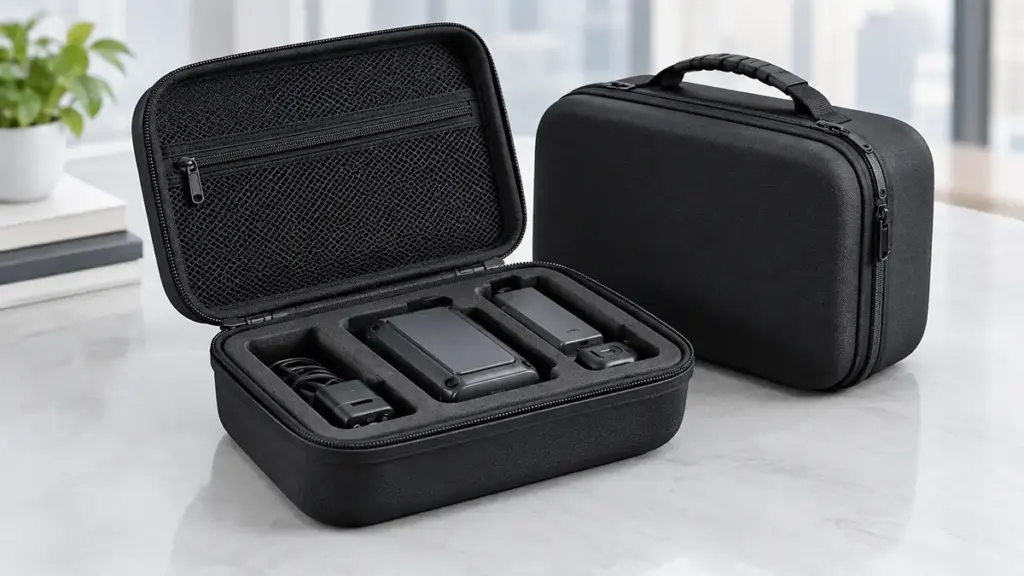
Generic, off-the-shelf enclosures offer lower upfront costs, but a vetted factory and a frozen specification are what protect your brand reputation against field damage. Calibrated foam density, controlled lamination, and reinforced stitching are what let high-value equipment survive harsh transit — while unvetted alternatives tend to surface later as returns and compromised client trust.
Secure a first-article production sample to evaluate structural tolerances and stitching quality firsthand, and share your 3D CAD files early: a technical blueprint review before tooling usually costs you two days of design feedback and saves a production run.